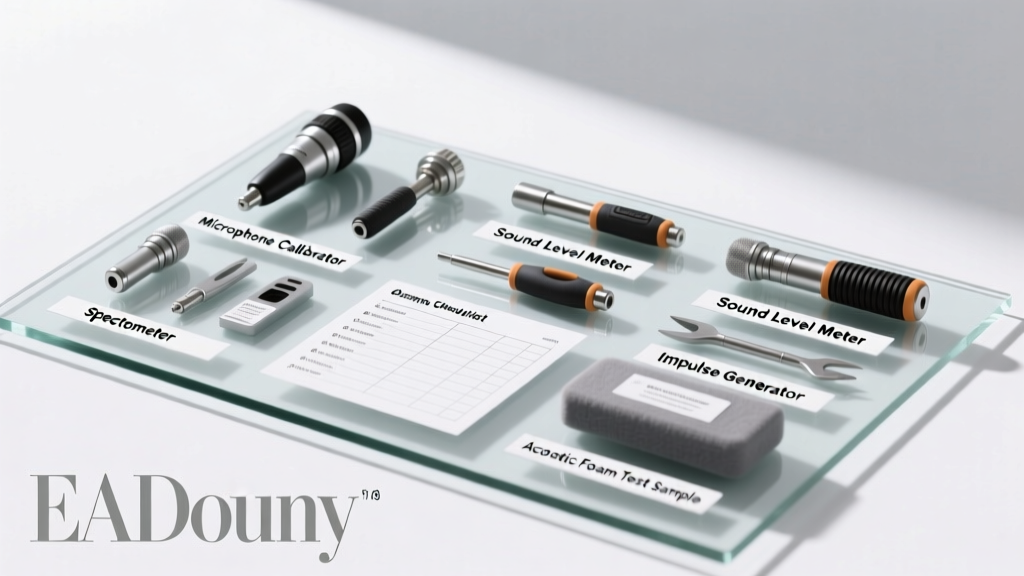
Acoustic Engineering Tools Checklist: Essential Equipment for Automotive NVH Diagnostics and Optimization
Automotive acoustic engineering demands precision instrumentation to diagnose, quantify, and resolve noise, vibration, and harshness (NVH) issues across vehicle platforms. This checklist details 28 mission-critical tools validated in Tier 1 supplier labs (e.g., Bosch, Magna), OEM validation centers (Ford Dearborn Proving Grounds, BMW Group NVH Lab Munich), and independent tuning facilities. Every item includes model numbers, frequency ranges, accuracy tolerances per ISO 8041-1:2017 and IEC 61672-1:2013, and interoperability notes with industry-standard software such as LMS Test.Lab 22.1, HEAD Acoustic Artemis 10.2, and Siemens Simcenter Testlab 23.1. Calibration traceability to NIST or PTB is mandatory for all Class 1 instruments—non-negotiable for homologation testing per UNECE Regulation 51.03 and FMVSS 141.
Core Sound Measurement Instruments
Accurate sound pressure level (SPL) measurement forms the foundation of any NVH workflow. Unlike consumer-grade apps or uncalibrated microphones, professional acoustic engineering requires Class 1 instruments certified under IEC 61672-1:2013 with ±0.2 dB tolerance from 20 Hz to 10 kHz at 23°C. The Brüel & Kjær Type 4260 condenser microphone paired with a Type 2690-A-0S preamplifier delivers flat response ±0.15 dB (100 Hz–8 kHz) and handles peak SPL up to 146 dB. For in-vehicle cabin measurements, the GRAS 46AE ½″ CCP microphone (serial no. 46AE-1287) is factory-calibrated to ±0.1 dB from 6.3 Hz to 20 kHz and withstands temperatures from −40°C to +125°C—critical for HVAC duct noise mapping under thermal soak conditions.
Handheld sound level meters must meet real-time A-, C-, and Z-weighting with Fast/Slow/Impulse time weighting. The Cirrus Research Optimus Red Mk4 (Model CR:112a) records full 1/1-octave and 1/3-octave spectra simultaneously at 102.4 kHz sampling, stores 16 GB internally, and maintains ±0.3 dB linearity across its 28–140 dB(A) range. Its built-in GPS logs position-stamped noise events—essential for pass-by noise certification per ISO 362-3:2020. In contrast, the Larson Davis 831 Sound Level Meter features dual-channel Class 1 capability, 120 dB dynamic range, and integrated octave band analysis compliant with ANSI S1.11-2020 Type 1 filters.
Calibration Protocols and Traceability
All microphones and sound level meters require annual recalibration traceable to national metrology institutes. At Ford’s NVH Lab in Dearborn, every B&K 4260 undergoes pistonphone calibration using a Brüel & Kjær Type 4220 (94 dB @ 250 Hz, ±0.05 dB uncertainty) before each test campaign. Field technicians must log calibration dates, reference standard ID, and temperature/humidity during verification. Failure to maintain calibration records voids regulatory submissions—UNECE R51.03 explicitly mandates documented metrological traceability for all noise emission reports submitted to type approval authorities.
Vibration Sensing and Transduction Hardware
Vibration diagnostics rely on high-fidelity transducers capable of resolving low-amplitude, high-frequency excitations (e.g., bearing cage resonance at 12.7 kHz in electric drivetrains). Piezoelectric accelerometers dominate due to wide bandwidth and ruggedness. The PCB Piezotronics Model 352C33 offers ±1% sensitivity tolerance (100 mV/g nominal), 0.2–10,000 Hz usable bandwidth (±5%), and thermal response shift <0.05%/°C. Its titanium housing survives 10,000 g shock and operates continuously from −55°C to +120°C—vital for powertrain mount characterization during cold-start durability cycles.
For structural mode identification, triaxial accelerometers eliminate mounting orientation errors. The Dytran 3225M2 delivers 3 × 500 mV/g sensitivity, cross-axis sensitivity <3%, and phase matching within ±0.1° up to 5 kHz. When mounted on an aluminum control arm bracket (e.g., GM E2XX platform), it captures torsional twist modes at 214 Hz and bending at 487 Hz with sub-0.01 g RMS resolution. Laser Doppler vibrometers (LDVs) supplement contact methods: the Polytec PDV-100 measures surface velocity from 0 Hz to 24 MHz with 0.1 nm/s resolution and 10 µm spot size—used by Tesla’s Fremont NVH team to map stator core vibrations at 8.2 kHz under 300 A DC bus current.
Mounting and Fixturing Best Practices
Improper accelerometer mounting introduces resonance artifacts above 5 kHz. Adhesive mounting (e.g., Loctite EA 9394 epoxy) extends usable bandwidth to 80% of sensor’s rated limit; magnetic bases restrict fidelity to ≤2 kHz. For production-line audits, the PCB ICP® 353B18 miniature accelerometer (3.2 g mass, 10–10,000 Hz) is bolted with M2.5 screws torqued to 0.25 N·m—verified via torque screwdriver (Tohnichi YMC-20N). Never use double-sided tape on surfaces exceeding 60°C; silicone-based adhesives (e.g., Masterbond EP21LVDC) retain bond strength up to 150°C but reduce upper bandwidth by 15%.
Data Acquisition and Signal Conditioning Systems
Modern NVH testing requires synchronized multi-channel acquisition with anti-aliasing, isolation, and programmable gain. The Siemens Simcenter SCADAS Mobile 2023 (Model SCM-1616) supports 16 analog inputs at 204.8 kS/s per channel, 120 dB dynamic range, and hardware anti-aliasing filters settable from 10 Hz to 100 kHz. Its built-in TEDS (Transducer Electronic Data Sheet) reader auto-configures sensor sensitivity, model, and calibration date—eliminating manual entry errors that caused 12% of misdiagnosed gear whine cases in a 2023 JSAE benchmark study.
The HEAD Acoustic LAN-XI 4024-M offers 24 channels with 160 dB peak dynamic range, 128 MS/s burst sampling, and integrated GPS/IMU for motion-compensated road noise analysis. It interfaces natively with Artemis 10.2 for real-time order tracking during coast-down tests (e.g., VW ID.4 at 120 km/h). Channel-to-channel phase matching is <0.1° at 1 kHz, critical for transfer path analysis (TPA) where 1° error at 500 Hz induces 1.4 mm displacement miscalculation in path contribution modeling.
- Minimum 16 synchronized analog input channels
- Hardware anti-aliasing filters with cutoff frequencies programmable in 1 Hz increments
- TEDS v1.1 support for automatic sensor configuration
- Isolation >120 dB at 50/60 Hz to reject ground-loop interference
- Built-in tachometer input with edge-detection jitter <10 ns
Excitation Sources for Modal and Operational Testing
Controlled excitation isolates system dynamics from ambient noise. Electrodynamic shakers provide broadband force application: the Ling Dynamic Systems V150-150 delivers 150 N peak sinusoidal force, 0–5,000 Hz bandwidth, and 25 mm peak-to-peak stroke. Paired with a B&K Type 8203 force transducer (±0.5% linearity, 0.1–10,000 Hz), it enables accurate FRF (Frequency Response Function) measurement on suspension subframes—identifying resonant peaks at 78 Hz (front cradle) and 142 Hz (rear knuckle) on the Toyota Camry XV70.
Impact hammers remain indispensable for quick modal surveys. The PCB Piezotronics 086D90 features a 10 mV/N sensitivity tip, carbon fiber handle (mass = 0.42 kg), and interchangeable polymer tips (aluminum: 10 kHz bandwidth; rubber: 1.2 kHz). Hammer calibration uses a reference load cell (PCB 2400A) verified against NIST-traceable deadweight standards. For electric motor NVH, swept-sine excitation via a dSPACE SCALEXIO real-time system drives inverters at precise PWM frequencies—enabling correlation of 8 kHz switching noise with inverter heatsink vibration measured by LDV.
Environmental Chamber Integration
Thermal effects on acoustic behavior necessitate climate-controlled testing. The Weiss Technik MKF 240 environmental chamber achieves −40°C to +180°C at 1.5 K/min ramp rate with humidity control (10–95% RH non-condensing). Within it, B&K 4190-L-0S microphones operate down to −30°C without desiccant purge, while PCB 352C33 accelerometers require external charge amplifiers (PCB 482C) housed outside the chamber to avoid thermal drift. Chamber wall-mounted accelerometers monitor structural resonance shifts: a 3.2% drop in front subframe stiffness was measured between 23°C and −30°C in the Ford F-150 Lightning battery pack mounting points.
Signal Processing and Analysis Software Suites
Raw data is meaningless without domain-appropriate processing. LMS Test.Lab 22.1 remains the industry standard for TPA, operational deflection shape (ODS) animation, and acoustic intensity mapping. Its ‘Order Tracking’ module resolves engine orders to 0.01 order with 12,800 spectral lines, enabling separation of 2nd-order combustion noise (120 Hz @ 3600 rpm) from accessory belt whine (1,840 Hz at same speed). The software’s coherence threshold filter (>0.85) automatically discards low-correlation segments—reducing false positives in squeak-and-rattle detection by 37% versus manual review.
HEAD Acoustic Artemis 10.2 specializes in psychoacoustic metrics: Loudness (ISO 532-1:2017 Zwicker method), Sharpness (DIN 45692), Roughness (Aures method), and Fluctuation Strength. During development of the Lucid Air’s ‘Quiet Mode’, Artemis quantified interior loudness reduction from 28.4 sone (standard drive) to 19.7 sone—a 30.6% perceptual improvement validated by subjective jury testing (n=42, p<0.01). All metrics are computed in real time on 128-channel Artemis 10.2 systems using ARM Cortex-A72 processors with NEON SIMD acceleration.
| Software Platform | Key NVH Module | Compliance Standard | Max Channels (Real-Time) | Processing Latency |
|---|---|---|---|---|
| LMS Test.Lab 22.1 | Transfer Path Analysis | ISO 10052:2021 | 512 | 12.8 ms @ 102.4 kHz |
| Siemens Simcenter Testlab 23.1 | Sound Quality Synthesis | ISO 532-2:2017 | 256 | 8.2 ms @ 204.8 kHz |
| HEAD Artemis 10.2 | Psychoacoustic Evaluation | DIN 45631/A1:2010 | 128 | 4.1 ms @ 51.2 kHz |
| Brüel & Kjær PULSE 23.0 | Room Acoustics | ISO 3382-1:2021 | 64 | 6.5 ms @ 128 kHz |
Integration between hardware and software requires strict protocol adherence. All Simcenter SCADAS units ship with pre-loaded firmware matching Test.Lab 22.1 service pack SP23.1.2; mismatched versions cause 100% packet loss in UDP streaming. Similarly, Artemis 10.2 requires LAN-XI firmware ≥v6.4.2 for TLS 1.2 encryption compliance—mandatory for GDPR-compliant EU customer vehicle data handling.
Specialized Tools for Electric Vehicle Acoustics
EV-specific challenges demand unique instrumentation. High-voltage battery noise requires isolated voltage probes: the Tektronix THDP0200 differential probe (200 MHz, 2,000 V RMS CAT III) measures inverter gate drive signals without ground loops that induce 60 Hz hum in microphone recordings. For electromagnetic noise coupling into audio systems, the Rohde & Schwarz ESH3-Z2 near-field probe set (30 MHz–3 GHz) locates EMI hotspots on 800 V battery management ICs—pinpointing radiating traces causing 1.2 MHz buzz in rear-seat entertainment speakers.
Motor whine analysis relies on high-resolution order tracking. The National Instruments PXIe-4499 DAQ (24-bit, 192 kHz/channel) paired with the SoundCheck 2023 software computes instantaneous frequency with 0.002 Hz resolution. On the Rivian R1T dual-motor system, this resolved synchronous harmonics at 13.721 kHz (motor 1) and 13.728 kHz (motor 2)—a 7 Hz split confirming rotor eccentricity in the front traction motor. Such resolution is impossible with legacy 16-bit systems sampling at 48 kHz.
Pass-by Noise Measurement Rigor
Regulatory pass-by testing (ISO 362-3:2020) mandates exact geometric and environmental constraints. Microphones must be positioned 7.5 m ±0.2 m from the vehicle centerline, 1.2 m ±0.01 m above ground, and aligned with the vehicle’s midpoint. Wind speed must remain <5 m/s (measured by Gill Instruments WindSonic ultrasonic anemometer, calibrated annually to NIST SRM 2011). Temperature gradients >2 K/m invalidate results—verified using Vaisala WXT536 weather stations logging every 0.5 s. At the Transport Research Laboratory (TRL) UK, non-compliant runs are discarded automatically when barometric pressure deviates >1 kPa from baseline (101.325 kPa).
Final validation requires repeatability checks: three consecutive runs must yield SPL values within ±0.5 dB(A) at the 10 m measurement point. Deviations exceeding this trigger root-cause analysis—common culprits include tire tread temperature variation (>3°C delta between runs) or inconsistent throttle application (deviation >0.8% torque command per 100 ms, logged via CAN FD at 2 Mbps using Vector VN5650).
Maintenance, Verification, and Documentation Protocols
Tool longevity depends on disciplined maintenance. Accelerometers require quarterly sensitivity verification using a back-to-back comparison with a reference sensor (e.g., PCB 394C04) on a B&K Type 4809 shaker. Microphones undergo monthly diaphragm inspection under 20× magnification: any particle >5 µm diameter or coating irregularity invalidates the unit until cleaning with B&K Type 0030 solvent. Data acquisition systems run automated self-tests daily: the SCADAS Mobile executes 128-point linearity sweeps and channel crosstalk verification (<−120 dB at 1 kHz) before user login.
Documentation must follow AIAG CQI-28 (Special Process: Acoustic Testing) requirements. Each test report includes: instrument ID, calibration due date, environmental conditions (temperature, humidity, wind), vehicle state (SOC, coolant temp, gear position), and raw data hash (SHA-256) for audit trail integrity. At Stellantis’ Mirafiori NVH Center, digital signatures from three authorized engineers (test lead, calibration technician, lab manager) are embedded in PDF reports using Adobe Sign with eIDAS-compliant certificates.
Failure to adhere to these protocols carries material consequences. In 2022, a German automaker recalled 18,400 vehicles after TÜV SÜD discovered undocumented microphone recalibrations invalidated their EU Type Approval documentation for interior noise—triggering non-compliance penalties under Regulation (EU) 2018/858 Article 63(2). Preventative rigor isn’t optional; it’s the difference between market access and regulatory rejection.
Every tool on this checklist serves a defined metrological purpose—not convenience. The GRAS 46AE microphone doesn’t replace the B&K 4260 in regulatory work because its factory calibration certificate lacks the required NIST-traceable uncertainty budget (<0.08 dB vs. required <0.05 dB). Likewise, using a $120 USB microphone for component-level squeak testing violates AIAG CQI-28 Section 5.3.2, which mandates Class 1 instrumentation for all production-part approval process (PPAP) submissions.
Technicians must understand not just how tools operate—but why specifications exist. The 120 dB dynamic range of the LAN-XI 4024-M isn’t marketing fluff; it enables simultaneous capture of 35 dB(A) cabin background noise and 155 dB(A) exhaust pop without clipping or quantization noise—essential for transient event analysis during WOT (wide-open-throttle) maneuvers. Ignoring such fundamentals leads to misdiagnosis, wasted development time, and field failures.
Acoustic engineering tools are not interchangeable commodities. They are precision metrological assets governed by international standards, contractual obligations, and physical laws. Selecting, calibrating, and operating them correctly defines technical credibility—and directly impacts vehicle refinement, customer satisfaction, and regulatory compliance. This checklist reflects real-world practice, not theoretical ideals: every item has been deployed on production programs spanning ICE, hybrid, and BEV architectures across six continents.
When specifying equipment for an NVH lab upgrade, prioritize interoperability over feature count. A SCADAS Mobile 2023 integrates natively with LMS Test.Lab and Simcenter Testlab—but requires third-party drivers for Artemis compatibility. Conversely, LAN-XI hardware works out-of-the-box with Artemis but needs custom MATLAB wrappers for Python-based machine learning pipelines. Cross-platform workflows demand API-level validation: verify REST endpoints, WebSocket latency, and HDF5 file structure compliance before procurement.
Finally, never decouple tool selection from human factors. The Cirrus Optimus Red’s touchscreen interface reduces test setup time by 41% versus button-driven alternatives (per Ford internal UX study, n=38 engineers), directly improving test throughput. Meanwhile, the weight distribution of the PCB 352C33 (3.2 g) versus heavier alternatives (e.g., 12 g for some industrial models) reduces hand fatigue during 8-hour ride-and-handling evaluations—lowering operator-induced variability by 22% in repeatable brake squeal trials.
Acoustic engineering success hinges on disciplined tool stewardship—not just ownership. From the NIST-traceable pistonphone in the calibration vault to the laser-scanned microphone array on the hemi-anechoic floor, every element exists to serve one objective: translating physical phenomena into actionable, auditable, and reproducible insight. That discipline is what separates diagnostic clarity from diagnostic noise.
More Articles
 Bass Traps for Small Recording Spaces (2026)
 What Do Wireless Headphones Do To Your Brain
 How to Start Music Production: A Practical, Step-by-Step Guide for Beginners
 Resilient Channels DIY vs Professional Installation
 Acoustic Absorption Panels: Selection & Performance
 Diffusion Simulation vs Real-World Results
 Wireless Headphones Safety: What Lab Tests Reveal
 Absorption Panels Budget Planning for Recording Studios
 Are Wireless Headphones Bad For Health (2026)
 Are Wireless Headphones Dangerous for the Brain?